
Warehouse Automation Solutions Supplier in India
From Storage to Automated Storage
At Ralbo Engineering Private Limited, we combine robust, precision-fabricated storage racking with modern automation technologies to build smarter, faster, safer, and more efficient warehouse operations. As a trusted warehouse automation solutions supplier in India, we help manufacturers, distributors, and logistics operators move beyond conventional racking to fully automated storage and retrieval systems (AS/RS).
Our automation solutions are engineered to optimise storage density, inventory accuracy, material movement, order fulfilment, and operational productivity, while reducing manual dependency and improving overall warehouse performance.
Why Warehouses Are Moving to Automation
Rising land costs, labour shortages, and the demand for faster order cycles are pushing Indian warehouses to rethink how they store and move goods. Conventional selective racking with forklift aisles typically leaves a large share of floor area and vertical height underused. Manual picking also introduces inventory errors and safety risks.
Automated storage systems address these challenges directly:
-
- Higher storage density through narrow aisles and deep-lane storage
- Full use of building height, often well beyond conventional forklift reach
- Real-time inventory accuracy via Warehouse Management System (WMS) integration
- Lower operating cost per pallet movement over the system lifecycle
- Improved safety by removing operators from high-level material handling
01 | Stacker Crane Automated Storage & Retrieval Systems (AS/RS)
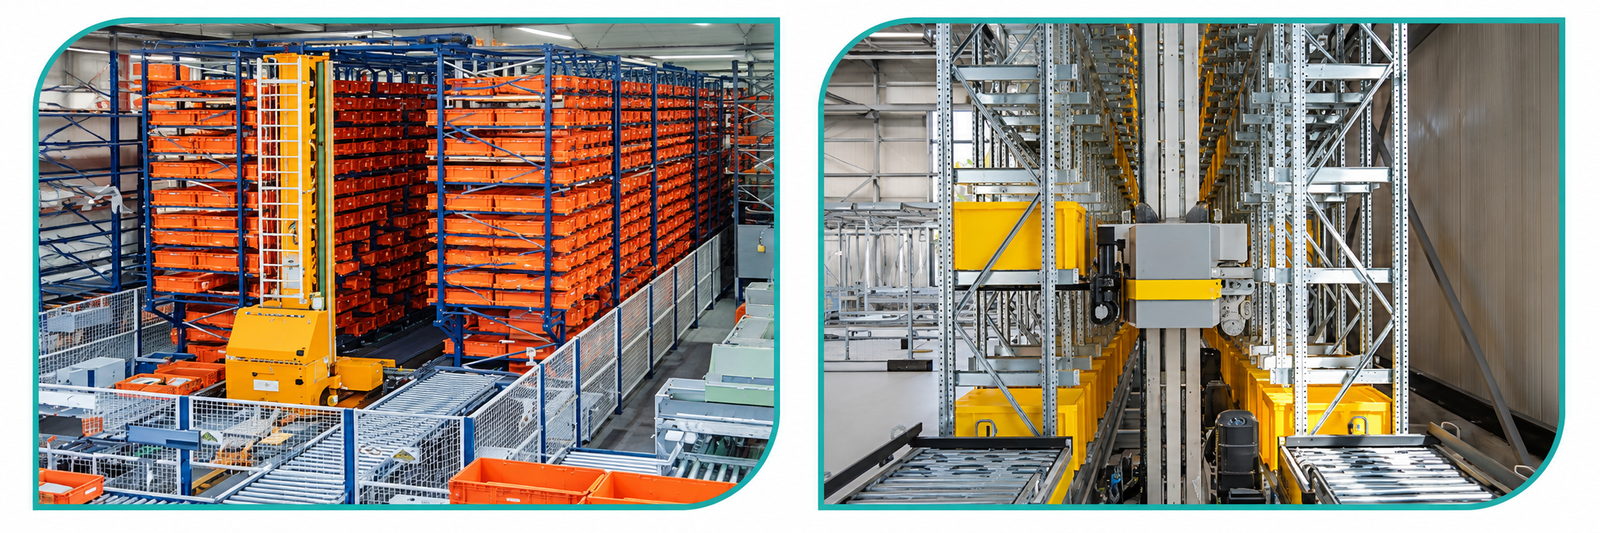
A Stacker Crane AS/RS is an automated warehouse storage system in which a rail-guided stacker crane stores and retrieves pallets or other loads from high-density racking according to computer instructions. The crane travels along a fixed aisle, lifts vertically, and uses a load-handling device to place or pull loads from rack locations — without human intervention.
Key Benefits:
-
- High-density storage with narrow aisle configurations
- Better use of warehouse height for vertical storage
- Reduced manual handling and forklift dependency
- Accurate, system-controlled inventory tracking
- Faster and more reliable storage and retrieval cycles
- Suitable for both pallet AS/RS and mini-load (tote/bin) AS/RS applications
Ideal for: High-throughput distribution centres, cold storage, automotive spares, FMCG, pharmaceuticals, and e-commerce fulfilment.
02 | Mother-Child Shuttle System
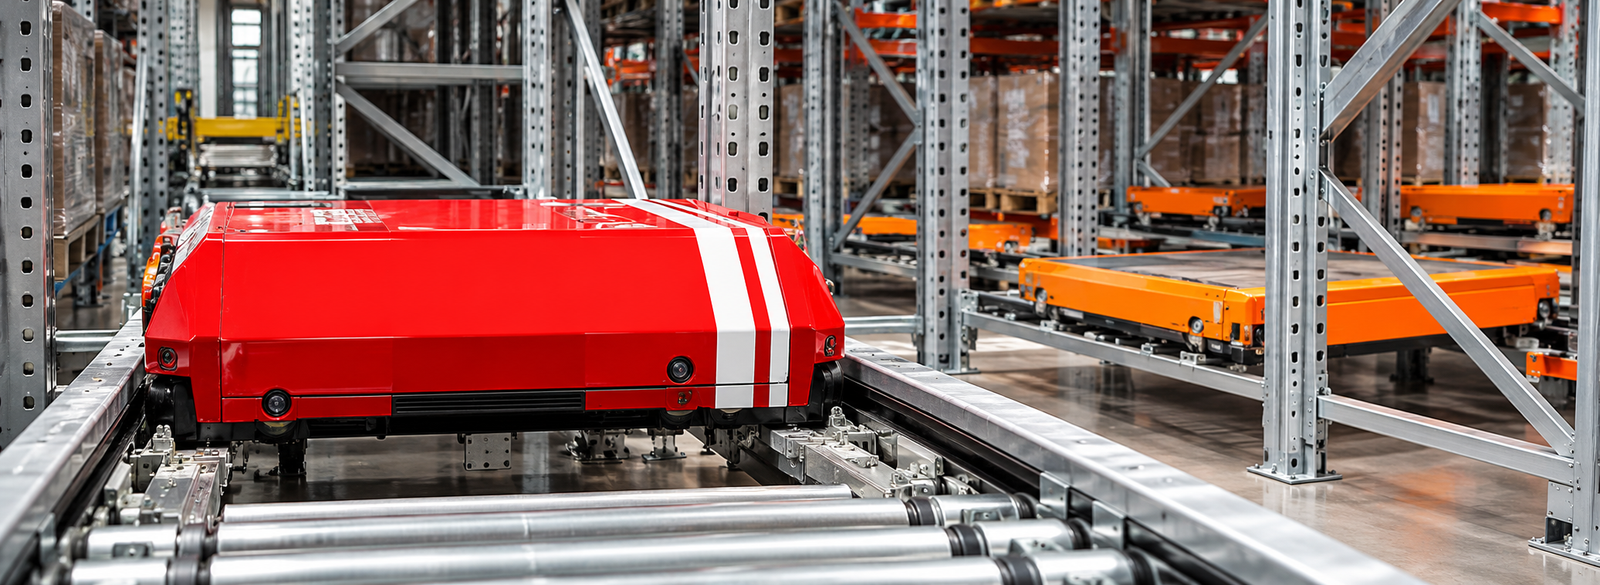
A Mother-Child Shuttle System is an advanced Automated Storage and Retrieval System (ASRS) that uses two coordinated robotic vehicles to store and retrieve goods in high-density warehouses.
-
- Mother Shuttle: A large primary carrier vehicle that travels horizontally along the main aisle or track, perpendicular to the storage lanes. It transports the child shuttle to the required storage location.
- Child Shuttle (Baby Shuttle): A smaller secondary vehicle that rides on the mother shuttle, detaches to enter individual storage lanes, and performs the actual lifting, placement, and retrieval of pallets.
In simple terms: the mother shuttle transports the child shuttle, while the child shuttle performs the storage and retrieval operation inside the rack.
Key Benefits:
-
- Very high storage density with deep-lane pallet storage
- Supports both FIFO and LIFO inventory management
- Minimal aisle space requirement
- Scalable — add shuttles as throughput grows
- Well suited to cold storage and bulk SKU environments
Stacker Crane AS/RS vs Mother-Child Shuttle — Which Fits Your Warehouse?
| Parameter | Stacker Crane AS/RS | Mother-Child Shuttle |
|---|---|---|
| Storage type | Single/double-deep | Deep-lane, high density |
| Best for | High SKU variety, high throughput | Fewer SKUs, large volumes per SKU |
| Height utilisation | Very high | High |
| Load types | Pallets and mini-load totes | Pallets |
| Scalability | Add aisles/cranes | Add shuttles/levels |
Our engineering team assesses your SKU profile, throughput, building dimensions, and load data before recommending the right system.
Why Choose Ralbo Engineering for Warehouse Automation
-
- Racking engineering expertise: In-house manufacturing of heavy-duty pallet racks, long-span racks, and mezzanine floors — the structural backbone of every automated system
- Structural integrity: Racking designed for the precise tolerances, load capacity, and deflection limits that automation demands
- Proven client base: Trusted by Tata Motors, Reliance, LG, Maruti, Northern Railway, and other leading organisations
- End-to-end support: Site survey, layout design, fabrication, installation, and after-sales service
- Manufacturing strength: Modern facility in Surajpur Industrial Area, Greater Noida, with 1000+ pieces monthly production capacity
Industries We Serve
Manufacturing plants · Warehousing & 3PL logistics · FMCG & food processing · Cold storage · Automotive & engineering · Pharmaceuticals · E-commerce fulfilment · Retail distribution
Request a Warehouse Automation Consultation
Furnish the Future with Ralbo Engineering. Contact our technical sales experts today at sales@ralbo.in or call +91-9953706842 to request a customized spatial audit and quote.
Ralbo Engineering Private Limited
A-2/2-25, Site B, Surajpur Industrial Area, Greater Noida – 201306 (U.P.)